Optional Analytics and Ads measure visits, forms and calls. Google forwarding can process call details. No form contents or personalized ads. You can still enquire if you reject. Read our privacy notice.
Recent AranVision work. Clients are not named and details that could identify them are left out; references can be discussed under NDA.
3 projects
Plastics
Plastics manufacturer — ongoing controls support
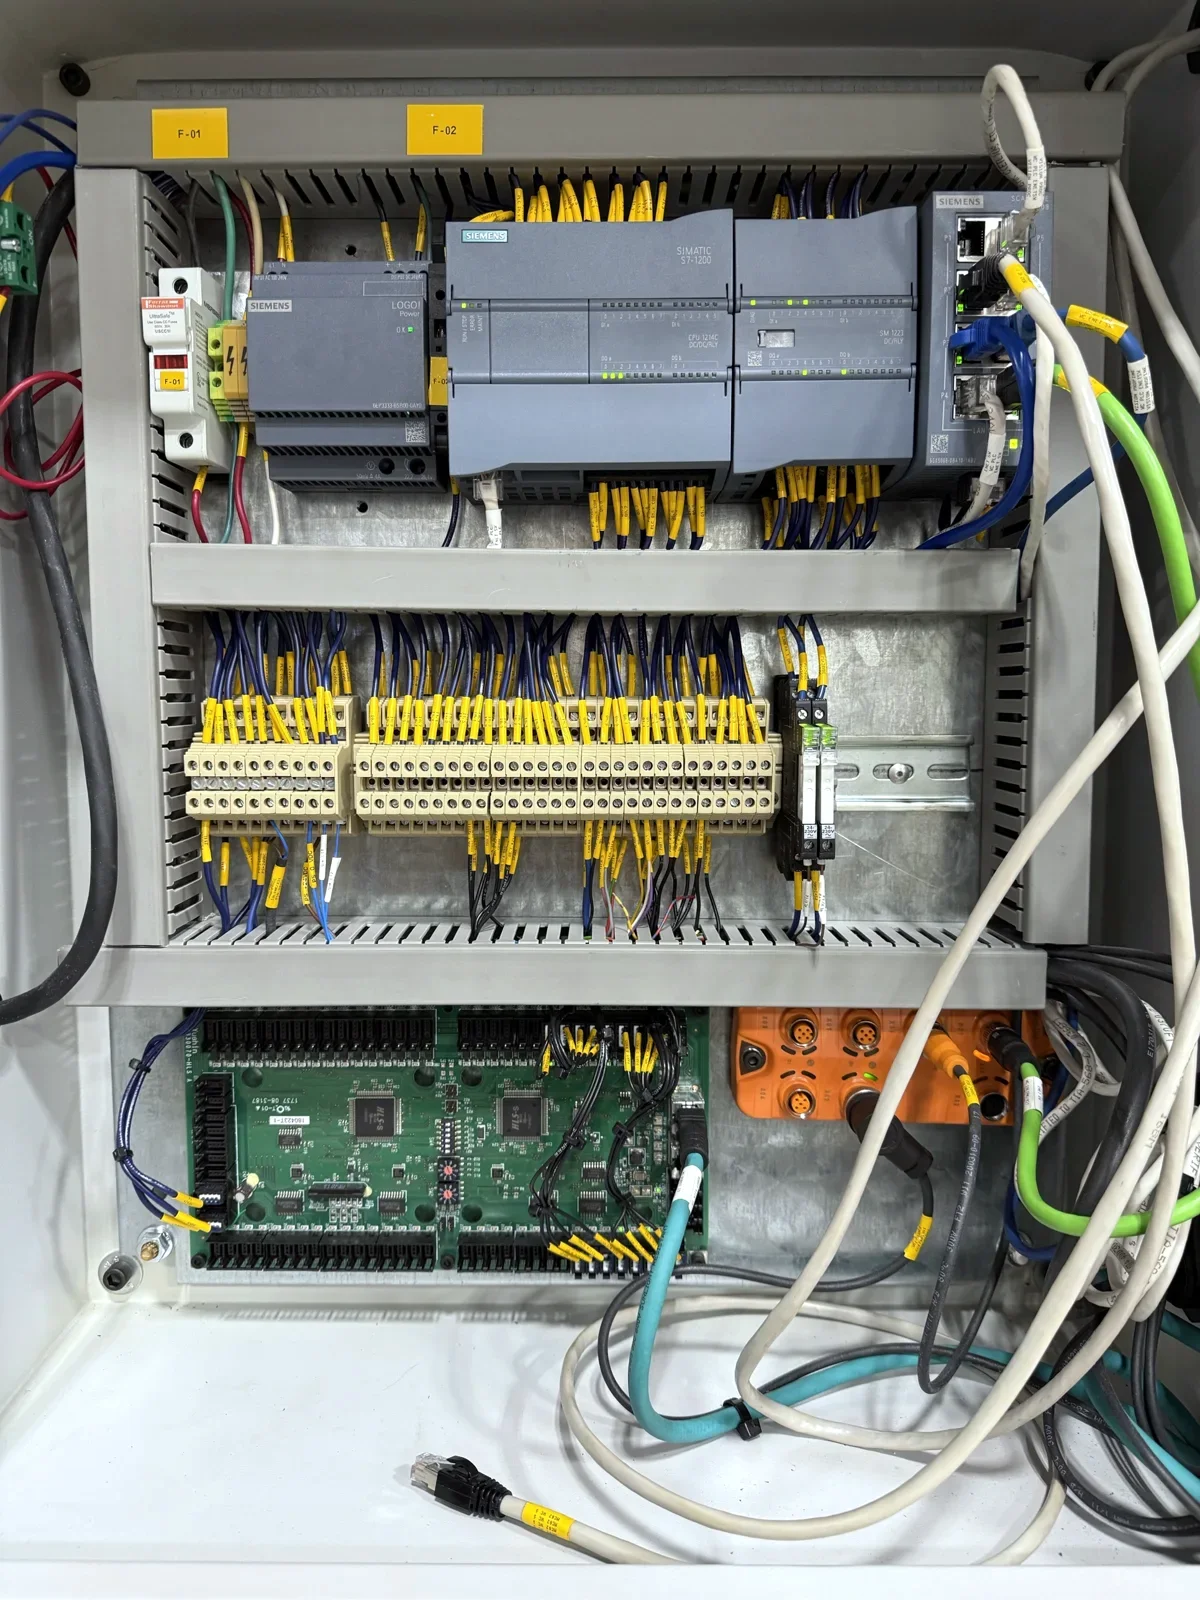
PLC, I/O and control-panel wiring
Problem
Controls for 15+ injection-moulding machines, robot workcells and post-mould assembly fixtures.
What AranVision did
TIA Portal upgrades of older Siemens programs (V13 to V19), new operator HMIs, robot-to-machine I/O and interlocks, cavity-pressure and vision-based part reject, swing-chute and mould-vacuum control, assembly-fixture logic, cycle timing captured on the HMI for production history.
Outcome
Machines kept in production with every change logged against the program revision history.
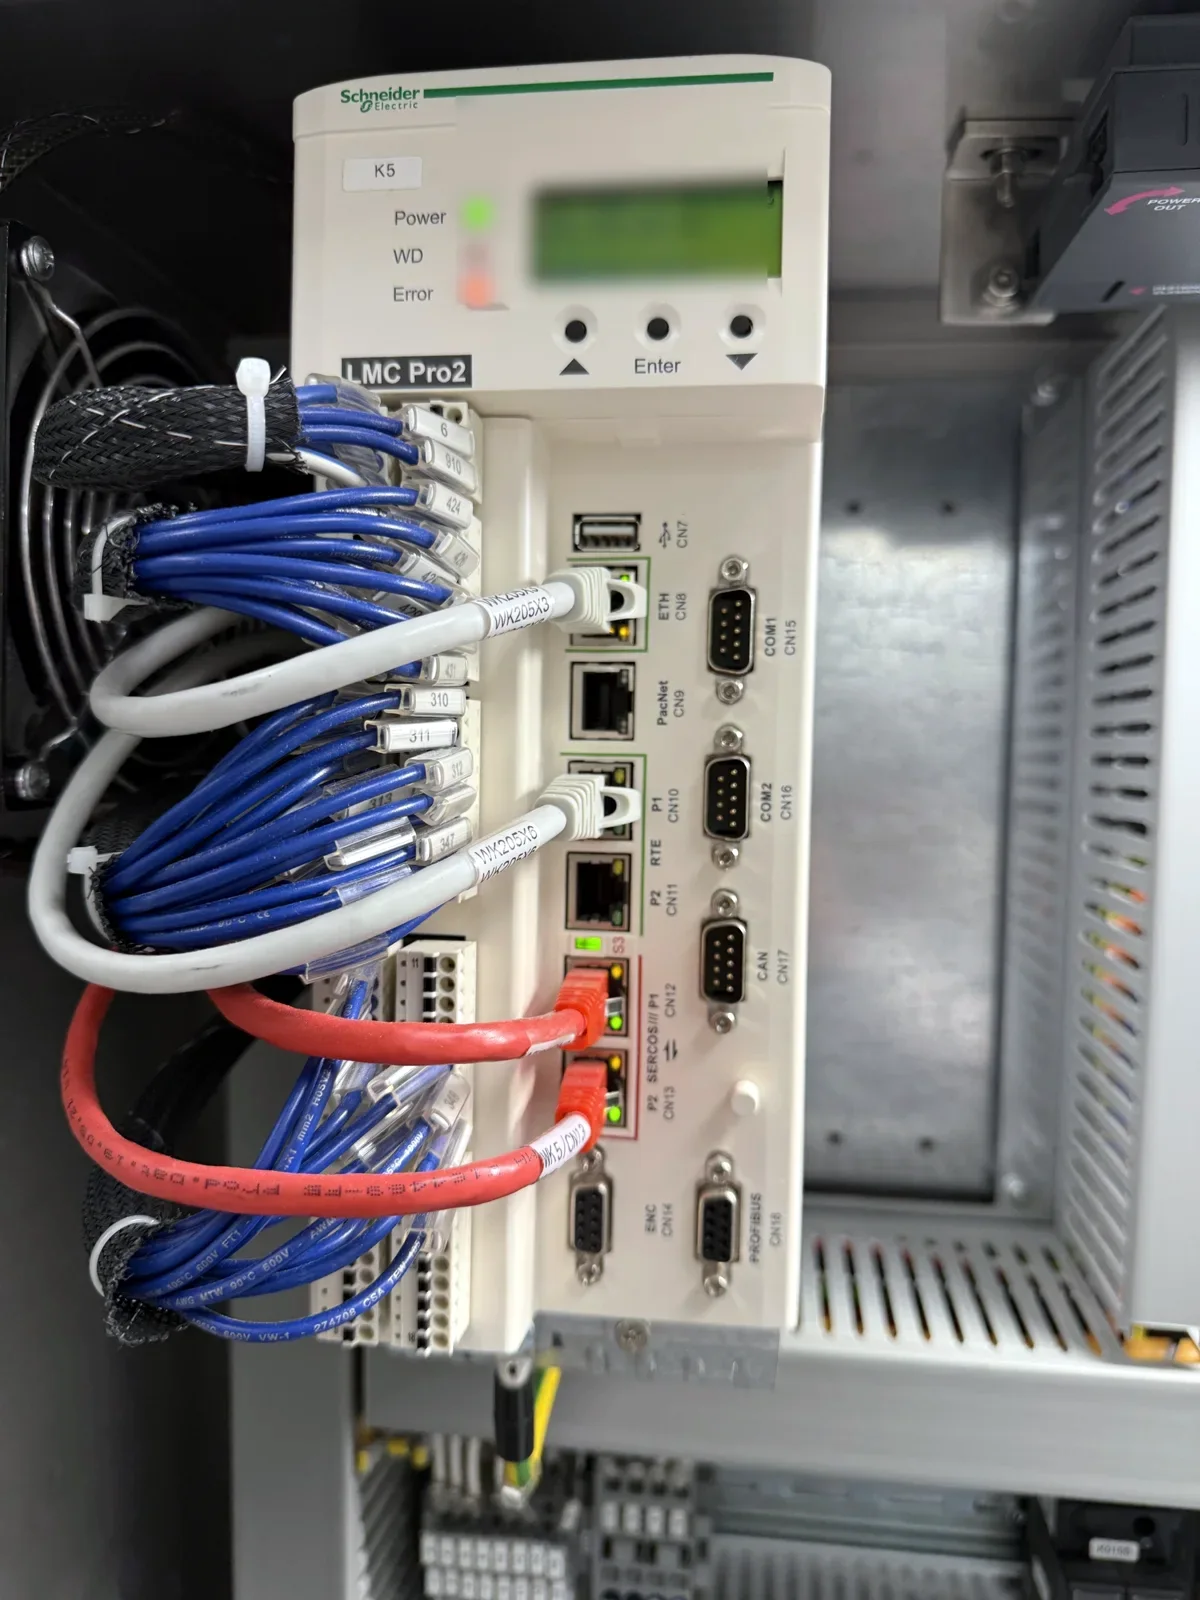
A servo-driven filling machine kept stopping mid-cycle.
What AranVision did
Traced the stop to the PLC sequence and corrected the sequence logic, then diagnosed and cleared the servo and sensor faults that showed up once the machine ran again.
Consumer-goods manufacturer — line would not start
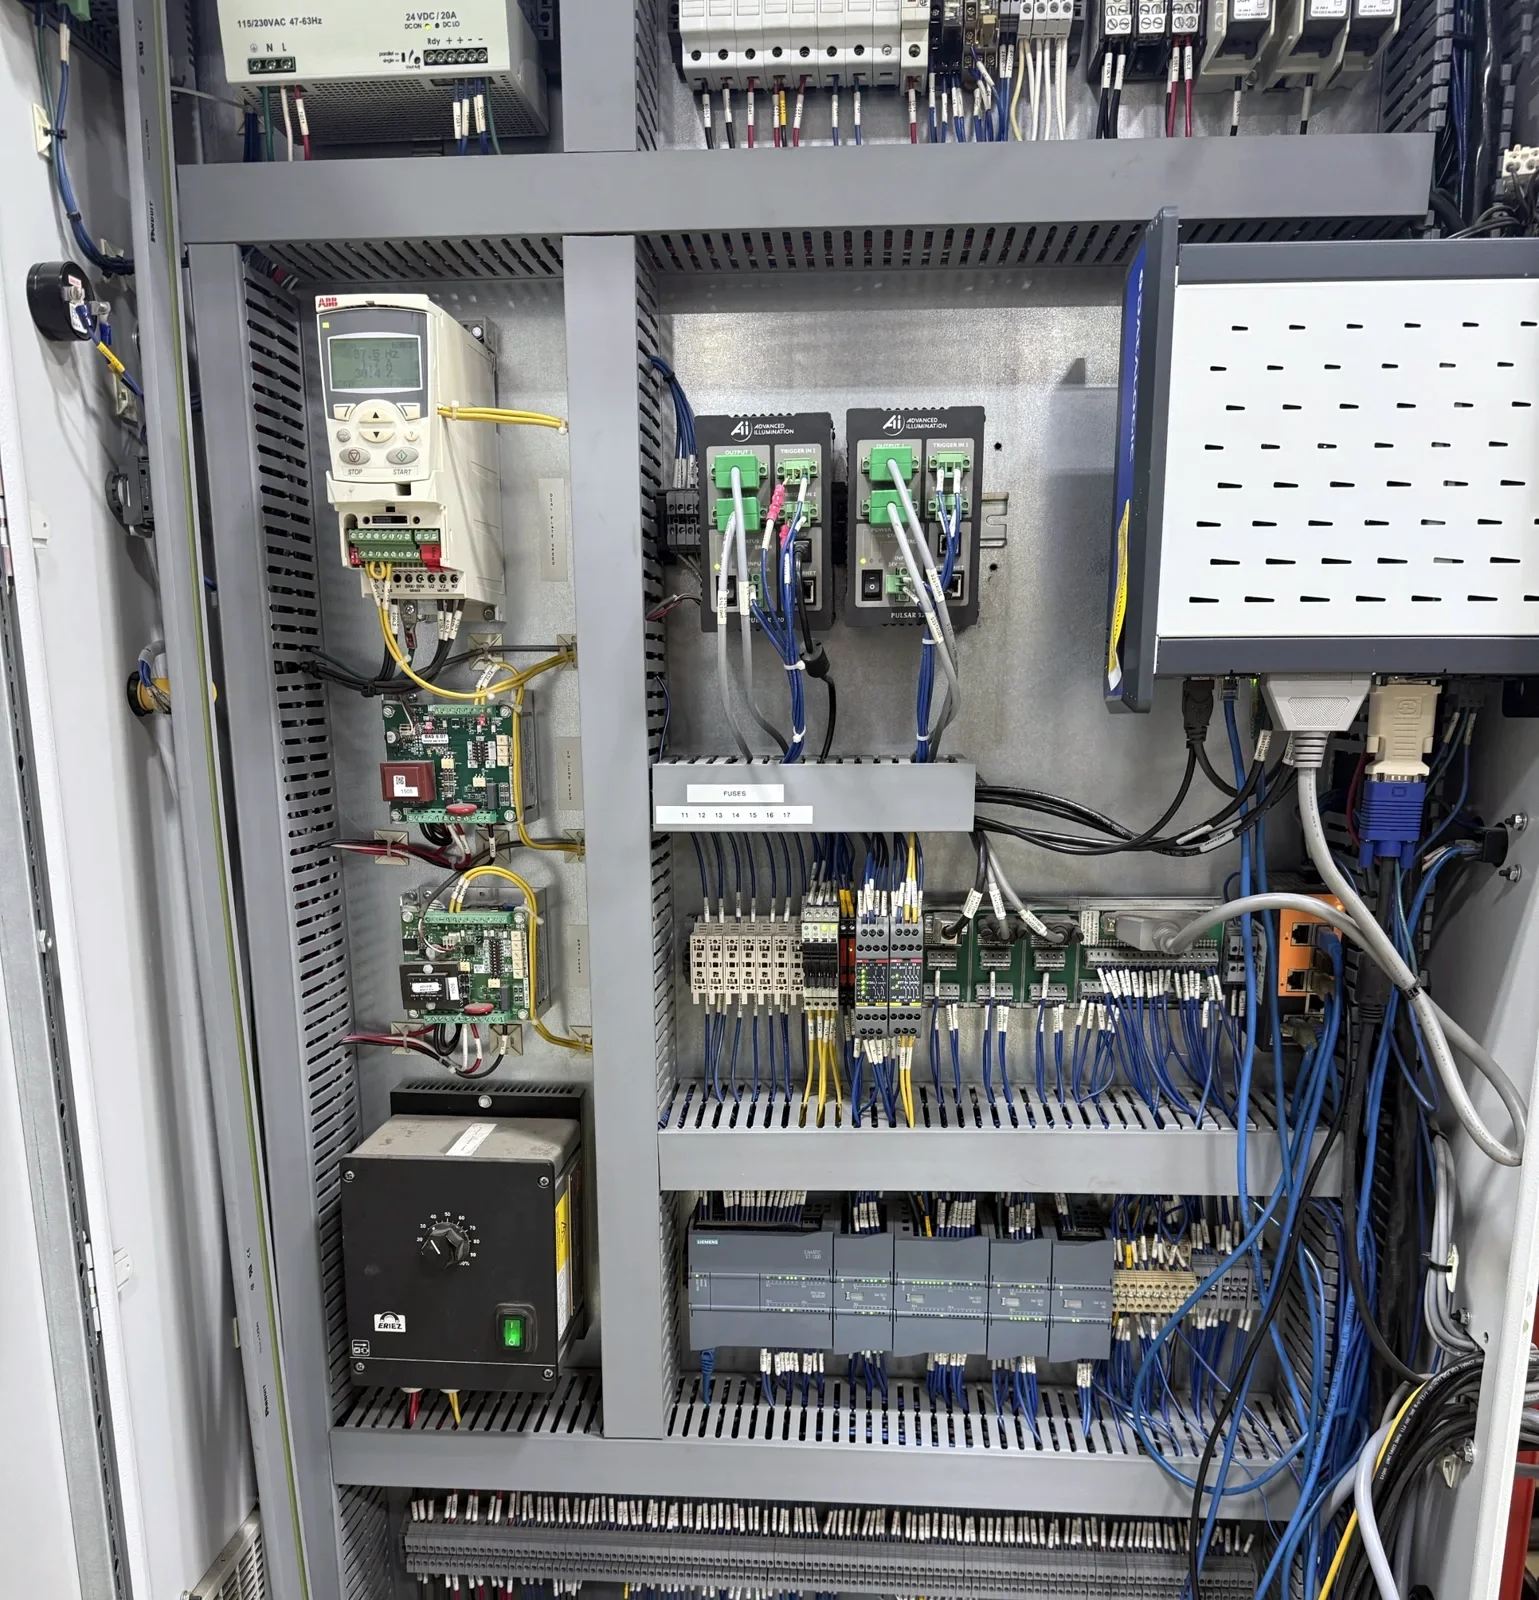
Control panel with drives and vision equipment
Problem
A blending and multi-scale weighing line would not start; production waiting.
What AranVision did
On-site diagnosis of the PLC, HMI and drives; full PLC program backup before any change.
Outcome
Start fault traced to a batch counter that had reached its target and was blocking the cycle; line restarted during the visit. Weighing instability on one scale documented with a follow-up test plan.