Optional Google Analytics and Google Ads measurement use advertising identifiers to measure site use and successful enquiries. Enquiry details are not included; personalized ads and enhanced conversions stay off. You can reject cookies and still enquire. Read our privacy notice.
Work that can be reviewed, tested and handed over.
AranVision supports new machines, production changes, legacy systems and defined programming work packages. The objective is not only working logic, but a control program that can be tested, diagnosed and supported after startup.
Siemens TIA PortalAllen-Bradley Studio 5000Beckhoff TwinCAT 3Schneider / CODESYSEtherNet/IPProfinet
Illustrative automation sequence
Sensor to controlled motion
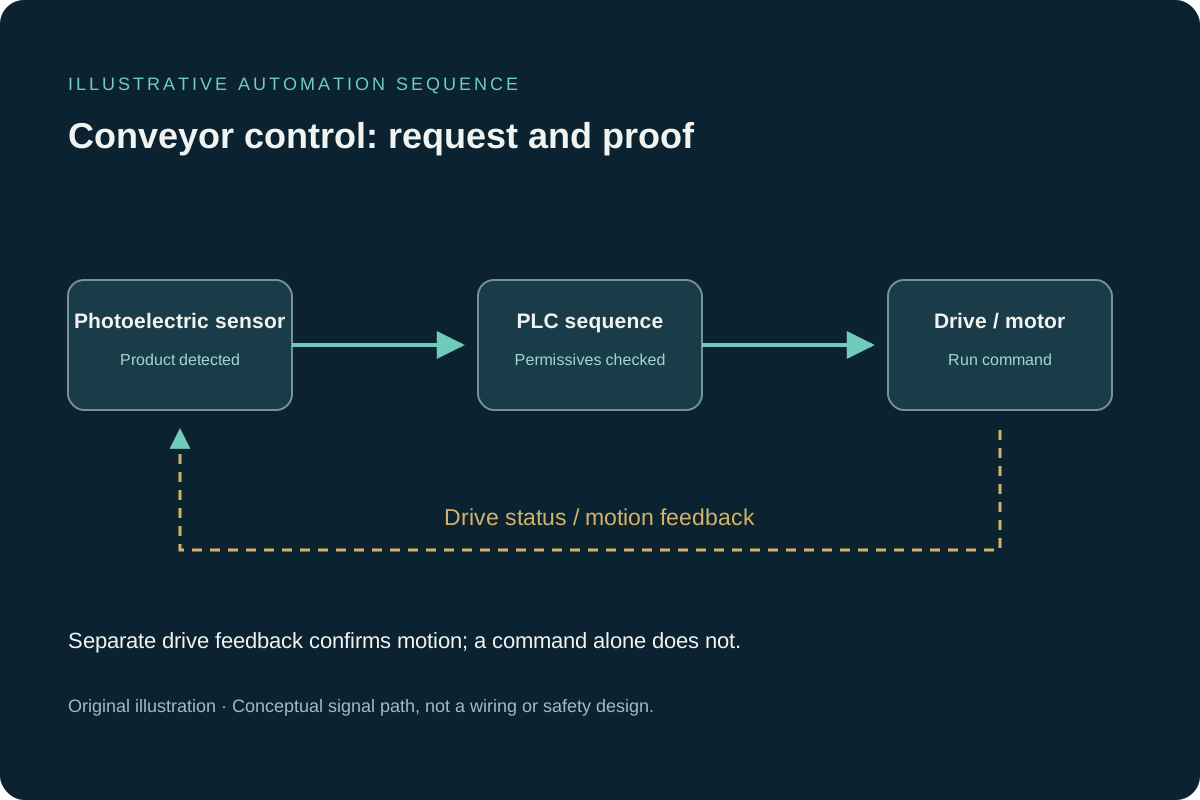
A product-position signal reaches the PLC. The controller commands a controlled motor stop at the inspection position.
Inspection: WAIT · Motor: running
1 Product approaching
2 Sensor detects product
3 PLC receives input
4 Motor stop command
5 Product positioned
View the control-signal diagramOriginal illustration. Conceptual signal path; a command is not confirmed feedback. Not a wiring or safety design.
Synthetic demonstration, not connected to plant equipment. Each 15-second cycle restarts the example. Sample inspection uses a fictional defect-area threshold of 15%; fruit colour is not a real quality assessment.
Illustrative automation sequence
Level-based pump control
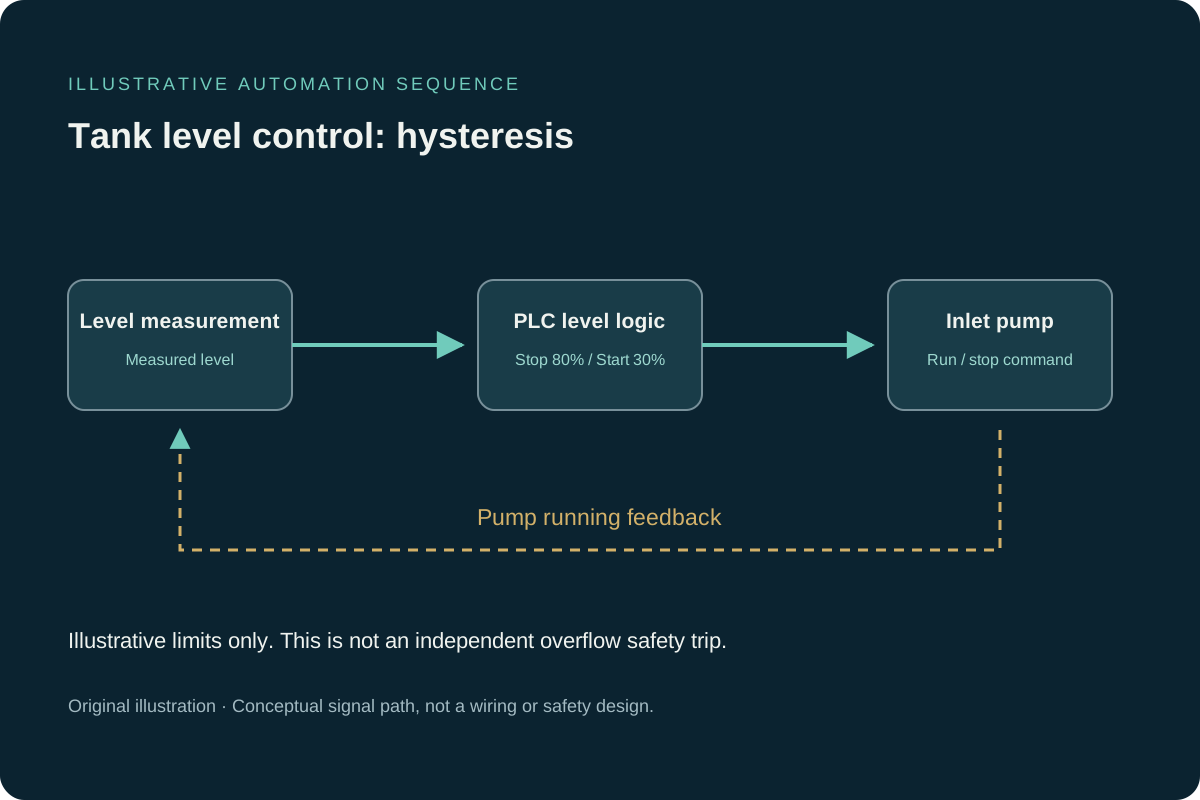
The inlet pump stops at 80% level and restarts at 30%. These illustrative thresholds demonstrate hysteresis, not a site-specific design.
Level: 30% · Pump: on
1 Tank filling
2 High level detected
3 Inlet pump stopped
4 Level falling
5 Pump restarted
View the control-signal diagramOriginal illustration. Conceptual signal path; a command is not confirmed feedback. Not a wiring or safety design.
Synthetic demonstration, not connected to plant equipment. Each 15-second cycle restarts the example. The 80% stop and 30% restart thresholds illustrate hysteresis; actual operating limits require site-specific design. The high-level warning illustrates process status; it is not an independent overflow safety trip.
Illustrative control example
More than a start command.
A coordinated pump sequence connects level conditions, pressure feedback, drive control and the operator interface. Watch the low-level stop and deliberate restart requirement in this example.
General industrial example, not installation footage. Values and timing are illustrative. The restart behaviour shown belongs to this example; actual requirements depend on the application. This is not a certified safety function or a performance claim.
Read the video transcript
A pump needs more than a start command. The tank level permits operation. The PLC enables the drive, and pressure feedback adjusts pump speed. If the level falls too low, the pump stops. Restoring the level does not restart it in this example. AranVision brings PLC logic, drives, instrumentation and operator interfaces together. Integration, modernization and commissioning in Toronto and the GTA. Discuss your project at aranvision dot C A.
Illustrative automation sequence
From a machine problem to coordinated controls.
Explore three examples of how sensing, control logic and confirmed feedback work together. AranVision supports new machine controls, system integration, modernization, commissioning and industrial data within an agreed project scope.
Consistent filling needs coordinated controls
A bottle-position signal permits a measured filling sequence. The valve closes before the nozzle retracts and the bottle is released.
Synthetic demonstration, not footage of an AranVision installation. Sequence and timing are illustrative; actual requirements depend on the application. These examples do not establish validated inspection performance or certified safety functions. Playback includes English narration, on-screen English captions and background music; choose Play to start. An optional English caption track is available in the player.
Read the video transcript
Consistent filling takes more than opening a valve. The bottle must be in position, the dose measured, and the valve closed at the right point. AranVision helps manufacturers solve industrial automation and controls challenges—from new machine controls and system integration to modernization, commissioning, and industrial data solutions. Explore what we can do for your production at AranVision dot ca.
Scope clarity
What a useful work package needs to establish.
PLC work begins by separating the requested change from the surrounding operating risk. Controller ownership, active program, firmware, I/O health, communication paths and safety boundaries are identified before code is changed. For an existing system, the current online state and available backups must agree or the discrepancy becomes part of the work package.
Logic is organized around observable states, explicit permissives and diagnosable faults. Offline development and simulation are used where practical, while final acceptance remains tied to the installed equipment. Downloads, forces and production tests require the client’s approved method, authorized personnel and a rollback decision.
Every engagement begins with a written boundary for access, production impact, client-supplied information, approvals and third-party responsibilities. Recommendations are tied to the evidence available at the time. If field discovery changes a critical assumption, the effect on scope, testing and acceptance is reviewed before the work proceeds.
Project readiness
Fit, inputs and acceptance before work starts.
These checkpoints keep responsibilities visible and prevent important interfaces from becoming late-stage surprises.
01
Best-fit assignments
A defined machine or process sequence that needs new logic, modification or fault correction
An OEM or integrator team that needs bounded programming capacity
An installed PLC where backups, access and a controlled test window can be established
02
Inputs to provide
Controller family, firmware, current program and communication method
Process narrative, I/O list, drawings and connected equipment information
Site standards, safety boundaries, outage window and approval responsibilities
03
Acceptance evidence
Online comparison and labelled as-left backup
Executed sequence, interlock, fault and restart tests
Recorded deviations, approved changes and handover notes
Project outcomes
What the engagement is designed to improve.
Clear sequence, interlock and alarm behaviour
Faster fault isolation during commissioning
Structured code and documented revisions
Controlled integration with drives, safety and field devices
Scope boundary
Programming, controls documentation, integration, testing and commissioning support are delivered within the agreed responsibility matrix. Any regulated professional engineering, electrical contracting, panel certification or authority approval is identified separately and assigned to the appropriately licensed or authorized party.
Typical deliverables
A defined package with clear technical outputs.
The final scope is adjusted to the installed system, project stage, client standards and site responsibilities.
01
PLC software development or modification
02
Sequence and interlock review
03
I/O mapping and device integration
04
Drive and axis command/feedback mapping within the agreed controller interfaces
05
Motion permissive, fault and controlled-restart test records
06
Offline testing and issue tracking
07
Commissioning support and as-left backup
08
Change summary and handover documentation
Delivery method
Three decisions that keep controls work under control.
01
Define the operating sequence
Confirm modes, states, permissives, interlocks, faults and recovery expectations before code changes begin.
02
Build for diagnosis
Organize logic, status and alarms so operators and maintenance teams can understand what is preventing operation.
03
Verify before production
Test normal sequences, abnormal conditions, communication loss and restart behaviour against agreed acceptance criteria.
Common questions
Questions to settle before kickoff.
Can you modify an existing PLC program?+
Yes. Work can begin with backup review, online comparison, I/O and network assessment, and a controlled change plan before implementation.
Can the work be delivered remotely?+
Design, code review and offline development can often be remote. Field checkout, startup and some troubleshooting require scheduled site access.